Press-brake test dies in PA6-CF
Use this record to plan and document experimental nylon-composite tooling. A printed die needs a defined load case and supported geometry; the material name alone does not establish capacity. Material profile: 3DP-034. No universal wall count, infill percentage or print temperature is specified for a load-bearing die.
What a die trial must record
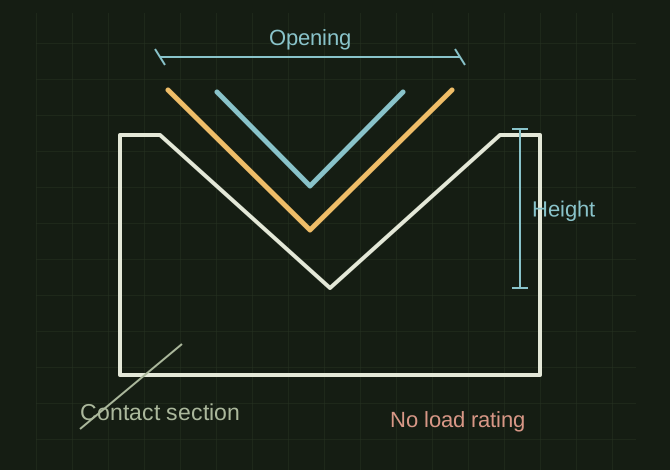 OPEN FULL SIZE ↗
- Material
- PA6-CF
- Concept height
- Roughly 3 inches; not a rating
- Capacity
- No tonnage or gauge established
TECHNICAL NOTES///
Use this record to plan and document experimental nylon-composite tooling. A printed die needs a defined load case and supported geometry; the material name alone does not establish capacity.
GOALRun the first test described in this guide and record the result for press-brake test dies in pa6-cf.
PREPARATION / NOTES
Material profile: 3DP-034. No universal wall count, infill percentage or print temperature is specified for a load-bearing die.
EQUIPMENT
- FDM printer / slicer
- Slicer project
- Calipers or inspection method
MATERIALS
- PA6-CF
STEPS
- Define actual sheet alloy, measured thickness, bend length, opening, punch radius and desired angle. Record the roughly 3-inch-tall concept as a design input, not a rating.
- Have the load path, machine setup and restraint reviewed by a qualified tooling person. Support the plastic against lateral spreading and keep layer interfaces out of the principal splitting direction where possible.
- Prepare PA6-CF using 3DP-034 and the exact spool datasheet. Print dimensional and bonding coupons before the die. Document orientation, walls, internal structure and drying history.
- Conduct any authorized machine trial under the shop’s guarded test procedure. Log force, stroke, angle, permanent deformation and cycle count; stop on cracking, delamination or shifting.
TROUBLESHOOTING
- SUNLU PA6-CF 20% was recovered from purchase context, but successful die tests were not. Follow the current exact-product guidance in 3DP-034 and verify the spool label. No tonnage or 16–10 gauge capability has been established.
SAFETY / LIMITS
- Use qualified judgment and current manufacturer or code guidance for safety-critical work.
THINGS TO WATCH FOR
SUNLU PA6-CF 20% was recovered from purchase context, but successful die tests were not. Follow the current exact-product guidance in 3DP-034 and verify the spool label. No tonnage or 16–10 gauge capability has been established.
RESULTA usable record includes before/after measurements and the actual tested load case. A single successful bend is not a production life rating.
DEVELOPMENT HISTORY///
Imported as an independent manifest record; public copy keeps uncertainty visible.
SPECIFICATION///
RELEASED MATERIAL///
A usable record includes before/after measurements and the actual tested load case. A single successful bend is not a production life rating.
The record keeps what is known at this revision. Unfinished tests stay unfinished here.