Adventurer 5M PLA retractable-wand profile
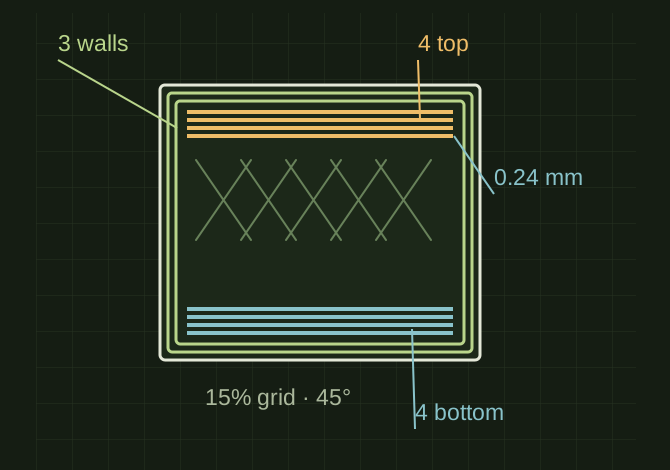
The current standard uses 0.24 mm layers, three walls, four top and bottom layers, 15% grid infill, 220°C first-layer / 215°C later nozzle temperature, 60°C first-layer / 55°C later bed temperature, controlled cooling, and a deliberately fast but bounded motion profile. It is a starting point for this printer, material, and nozzle combination—not a universal profile.
What the wand profile actually builds
 OPEN FULL SIZE ↗
- Layer
- 0.24 mm
- Perimeters
- 3
- Top / bottom
- 4 / 4
- Grid infill
- 15% at 45°
TECHNICAL NOTES///
Canonical fast-PLA starting profile for the retractable wand on a 0.4 mm nozzle.
GOALProduce a fast, strong retractable wand while preserving a reliable first layer.
EQUIPMENT
- Adventurer 5M
- 0.4 mm nozzle
- Slicer project/profile export
MATERIALS
- Standard PLA
STEPS
- Confirm printer, nozzle, material, and plate surface.
- Enter the starting values and keep the first layer conservative.
- Print a small motion/strength test before a full wand.
- Record the finished result and the next revision.
TROUBLESHOOTING
- A slicer preview is not proof that a finished part will fit or move.
- Change one process variable at a time so the next result is attributable.
- Keep material identity and nozzle size with every saved revision.
SAFETY / LIMITS
- Keep hot-end and moving-machine precautions in force.
- Validate strength and motion before treating the part as finished.
RESULTCanonical starting point; one confirmation print still validates the setup.
DEVELOPMENT HISTORY///
Imported as an independent manifest record; public copy keeps uncertainty visible.
SPECIFICATION///
RELEASED MATERIAL///
Canonical starting point; one confirmation print still validates the setup.
The record keeps what is known at this revision. Unfinished tests stay unfinished here.