A conversation-specific public summary of printing nylon on adventurer 5m, distilled from the supplied export. The detailed excerpts remain available in the released note file.
CHAT-0277REV EXPORT-03
AI narration using Robert's voice. Printing nylon on Adventurer 5M / short introduction.
Conversation-specific knowledge extracted from the printing nylon on adventurer 5m discussion.
EXTRACTED KNOWLEDGE / HOW-TOFROM CONVERSATION
QUESTION / CONTEXTTell me about printing with nylon on an adventurer 5m
RETAINED REPLY
--
The Adventurer 5M is a Core XY, enclosed 3D printer rated for high-speed printing and “high-temperature” materials (its hotend is specified up to ~280 °C) according to product specs. [embedded media omitted]
There is an optional enclosure kit for it (which is a big plus when printing hygroscopic or warp-sensitive materials). [embedded media omitted]
The machine’s integrated features (auto-leveling, enclosed build chamber, higher nozzle temperature) make it a better candidate for engineering-filaments than typical hobby printers.
Moisture absorption – Nylon is very hygroscopic. If it absorbs moisture, you’ll get bubbling, oozing, stringing, weak layers, and clogs. [embedded media omitted]
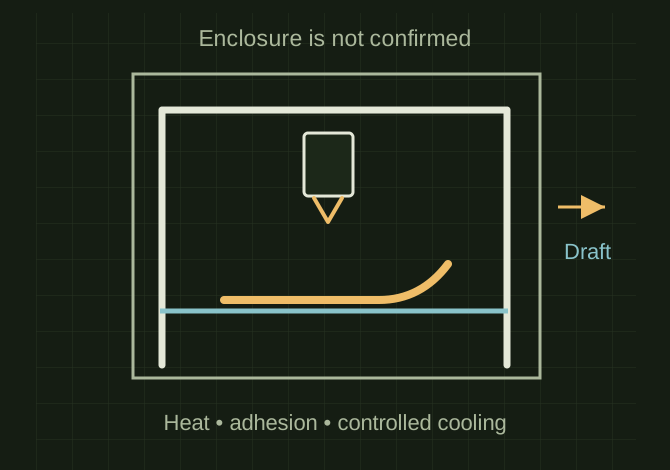
Warp / adhesion issues – Nylon tends to shrink and warp, and requires good bed adhesion + stable chamber temperature.
High temperature / slow cooling – High extrusion temps, minimal fan cooling for many nylon types, and appropriate retraction & ooze controls.
Stringing / ooze – Because nylon stays molten a bit longer and is more pliable, you’ll often see stringing if retraction & travel are not tuned. [embedded media omitted]
Extracted from the conversation’s assistant responses and edited for public clarity. See the released note for additional redacted excerpts.
DEVELOPMENT HISTORY///
2025.11.21EXPORT-04
Matched to the supplied export; key guidance is surfaced separately and the raw transcript remains unpublished.
 OPEN FULL SIZE ↗